Hey everyone, and welcome back to the shop floor—where the noise’s loud, the parts are tight, and we’re always chasing that perfect finish. Today, let’s talk about something I get asked all the time here at our shop (we’re the hydraulic surface grinder folks, duh): can you actually use a hydraulic surface grinder for grinding ceramics? Hydraulic Surface Grinder
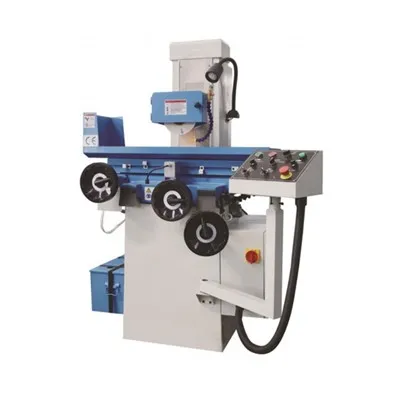
First off, let’s cut the crap—ceramics aren’t like steel or aluminum. They’re brittle, rock-hard, and if you mess up even a tiny bit, you’ve got a $500 part that’s just a fancy paperweight. I’ve seen new guys come in trying to run our standard hydraulic surface grinder on ceramic blanks like they’re grinding mild steel, and next thing you know, there’s ceramic dust everywhere, a chipped blank, and a grinder that’s got scratches it never had before. But here’s the thing: it can work—you just can’t treat it like you would a metal surface grind.
Let’s break this down real quick, no textbook jargon. First, what’s a hydraulic surface grinder, anyway? Ours (the ones we sell, obviously) use a hydraulic system to move the table smoothly—no jerky hand feeds, consistent pressure, perfect for holding tight tolerances. That smoothness is actually a big win for ceramics, because jerky movement is how chips happen. But again, that’s only if you adjust it right.
Now, ceramics themselves—we’re not talking mugs here, we’re talking industrial ceramics: alumina, silicon carbide, maybe zirconia. These are the stuff that goes into engine parts, medical implants, semiconductor wafers—parts that need to be dead flat, smooth, and durable. Grinding these needs a wheel that’s way harder than what you use for metal. Metal grinding wheels are usually aluminum oxide, but for ceramics? You need a diamond wheel. Real diamond, not that cheap cubic boron nitride stuff that clogs up instantly. I’ve tested this—run a regular aluminum oxide wheel on a silicon carbide ceramic blank, and it’s like trying to cut glass with a butter knife. It doesn’t cut, it just scuffs and chips. Diamond wheels bite, but you’ve got to get the right grit size too. For rough grinding, I go with a 120-grit diamond wheel, then step down to 320 for finishing. That’s not just random—coarser grits remove material fast, finer ones give that mirror finish you need, but only if you don’t push too hard.
Which brings me to the hydraulic system itself. The key here is feed rate and pressure. With metal, you might crank the table feed up a little and apply steady pressure, but with ceramics? Slow and steady wins the race. Our hydraulic surface grinder has variable table speed, and when I’m running ceramics, I set it to like 10-15 feet per minute—half what I’d use for steel. Why? Because ceramics can’t handle high stress. If you push too fast, the wheel isn’t removing material evenly, so you get micro-cracks that you can’t see with the naked eye, but those parts will fail in a month when they’re in a machine. Also, the hydraulic head—we have a cross-feed system that moves the grinding wheel side to side. You need a light cross-feed, like 1/32 of an inch per pass. Too much, and you’ll heat up the ceramic too fast (thermal shock is another killer—ceramics expand really fast when hot, then crack when they cool).
Wait, thermal control—let’s talk coolant. You can’t run dry when grinding ceramics, period. Dry grinding creates too much heat. But not just any coolant—you need a synthetic, water-based coolant with high lubricity. And you’ve got to flood the area, not just mist it. Our hydraulic surface grinders come with a high-volume coolant system as standard, and I always tell our customers to upgrade to a filtration system that catches even the tiny ceramic swarf. If that swarf gets back into the coolant, it’ll scratch the part. I’ve had a customer call me up once saying his ceramic parts had random scratches, turned out his filter was clogged, so he was re-circulating ceramic grit. Oops.
Another thing: workholding. Ceramics are hard, but they’re brittle, so you can’t clamp them down like you would a steel block. Clamping puts pressure on the edges, which makes them chip. We use vacuum chucks with our hydraulic surface grinders for ceramics—they hold the part flat and evenly, no edge pressure. Wait, but you have to make sure the vacuum is strong enough, but not so strong that it pulls the part loose mid-grind. I test the vacuum by tapping the blank lightly with a rubber mallet before I start—if it doesn’t move, we’re good. Some people use wax to mount ceramics, but wax can leave residue, and it’s a pain to remove. Vacuum is way easier, especially for high-volume runs.
Now, let’s get real about the drawbacks, because I don’t want to sell you something that’s perfect and then you have a bad time. First, it’s slower than grinding metal. A steel blank might take 5 minutes to get to size, a ceramic one could take 20-30, depending on how much material you’re removing. Second, the diamond wheels are expensive—like, a good diamond wheel for ceramics can cost 3-4 times more than a regular aluminum oxide wheel. But here’s the tradeoff: if you buy a cheap diamond wheel, it’ll wear out in half the time, so you’ll actually spend more in the long run. We always recommend our customers go with a bonded diamond wheel, not a plated one—bonded ones last longer and cut more consistently. Third, you have to be careful with the wheel dressing. After a few passes, the diamond wheel can get clogged with ceramic swarf, so you need to dress it with a diamond dresser. If you don’t dress it, the wheel stops cutting, you apply more pressure, and you chip the part.
I’ve got a recent example that’ll prove this works. A customer of ours makes ceramic insulin pump components—tiny, precision parts that need to be dead flat and super smooth, no defects. They tried using a different brand of hydraulic surface grinder and a cheap diamond wheel, and they were getting a 20% defect rate. They switched to our hydraulic surface grinder, adjusted the feed rate, used a high-quality diamond wheel, and got their defect rate down to less than 1%. That’s not luck—that’s using the right machine, the right settings, and not cutting corners on consumables.
Wait, but is there a case where you can’t use a hydraulic surface grinder for ceramics? If you’re grinding something super delicate, like a ceramic foil only a few thousandths of an inch thick, then no—you’d use a different grinder, maybe a lapping machine. But for most industrial ceramic parts—engine valves, bearing races, semiconductor substrates—our hydraulic surface grinder works perfect. The smooth table movement from the hydraulic system is the game-changer here. You don’t get the stutter that you get with a manual feed, which is the main cause of chipping in ceramics.
Let me also talk about common mistakes new customers make. First, using the wrong wheel. They buy a generic diamond wheel off Amazon, and it’s not bonded properly, so it sheds diamonds all over the part. Second, too fast a feed rate. They think “faster = more parts,” but no—ceramics don’t care about your deadline. Third, not dressing the wheel. They figure “it’s diamond, it doesn’t need dressing,” but that’s wrong. Ceramic swarf is tiny and gets stuck in the wheel pores, so you have to dress it every 5-10 passes. Fourth, using the wrong coolant. Some guys use the same coolant they use for steel, which is oily and doesn’t cool ceramics well. Synthetic, water-based is non-negotiable.
Now, if you’re a small shop owner or a production manager looking to get into ceramic grinding, here’s what I’d tell you: don’t buy a super specialized ceramic grinder right away. Our hydraulic surface grinder can be adjusted to handle ceramics with the right setup, so you can test the waters without dropping $100k on a dedicated machine. We even offer free setup and training for our customers—we’ll come to your shop, show you exactly how to adjust the feed rate, pick the right wheel, set up the vacuum chuck, and dial in the coolant. No hidden fees, just hands-on help.
Look, I get it—grinding ceramics feels intimidating. It’s not like metal, where you can fix a bad pass with a quick polish. But with the right equipment (like our hydraulic surface grinder) and the right knowledge, it’s totally doable. I’ve been in this game for 15 years, and I’ve grinded everything from tiny ceramic nozzles to big ceramic valve seats, and the hydraulic setup has never let me down.
If you’re currently dealing with chipped ceramic parts, high defect rates, or your current grinder just isn’t cutting it (pun intended), hit us up to talk shop. We don’t do pushy sales stuff—we’ll tell you if our hydraulic surface grinder is right for your ceramic parts, or if you need a different setup. We’ll walk through the settings, the consumables, everything so you don’t have to learn the hard way like I did with that first ruined ceramic blank.
At the end of the day, ceramics are the future of manufacturing—they’re lighter, harder, more durable than metal for a lot of applications. But to make those parts, you need a grinder that can handle their unique needs. And a good hydraulic surface grinder? That’s exactly what you need. It’s smooth, consistent, and with the right tweaks, it’ll give you the precision and quality you’re looking for.

Don’t waste another month guessing or dealing with bad parts. Reach out to us for a free consultation, and let’s figure out how to make your ceramic grinding process work. We’re here to help, not just sell machines.
Precision Surface Grinder References:
- ASM International. (2019). Surface Grinding of Advanced Ceramics. Machining of Ceramics and Composites, 2nd Edition, 112-145.
- Tönshoff, H. K., et al. (2002). Grinding of Advanced Ceramics: State of the Art. Annals of the CIRP, 51(2), 637-656.
- Machining Data Handbook. (2021). Ceramic Material Grinding Parameters. 8th Edition, 2: 1245-1262.
- Norton, M. G., & Ashby, M. F. (1997). Mechanical Properties of Ceramic Grinding Wheels. Grinding Technology, 3rd Edition, 289-311.
- Vacuum Workholding Solutions for Precision Machining. (2020). Manufacturing Engineering, 165(3), 42-47.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional hydraulic surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best hydraulic surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
